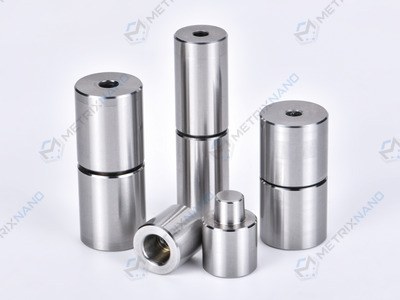
Core Mold Components for Automotive Security Lens Barrels MANUFACTURINGCore Mold Components for Automotive Security Lens Barrels
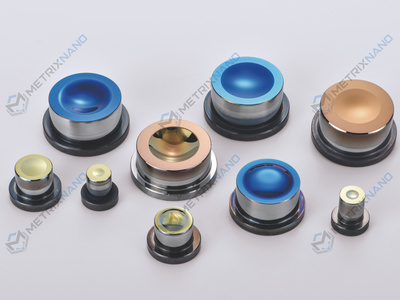
Threaded Core Pin · Lead Screw · Thread Guide Plate · Cavity Insert · Core PinThe lens barrel is a critical structural component in automotive security camera optical modules, and its mass production relies on precision injection molds. Within a lens barrel mold system, five key components — the threaded core pin, lead screw, thread guide plate, cavity insert, and core pin — work in coordination to directly determine the molding precision and yield of the lens barrel.
Five Components, Each with a Defined Role
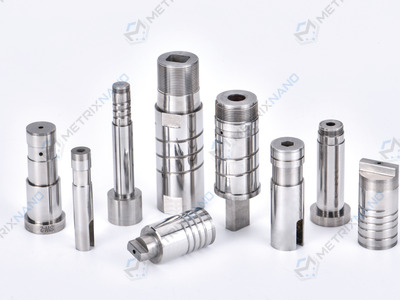
Threaded Core Pin — Forms the internal threads of the lens barrel. Made of S136 tool steel, heat-treated to HRC 56. Thread precision directly determines focusing engagement quality.
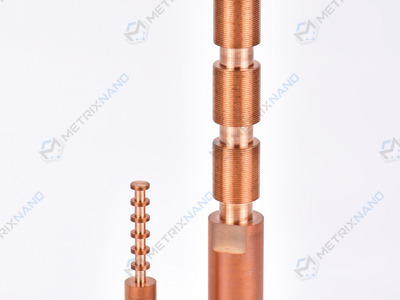
Lead Screw — Drives the rotary unscrewing mechanism for demolding. Lead accuracy must remain stable across hundreds of thousands of molding cycles. Surface nitriding treatment applied.
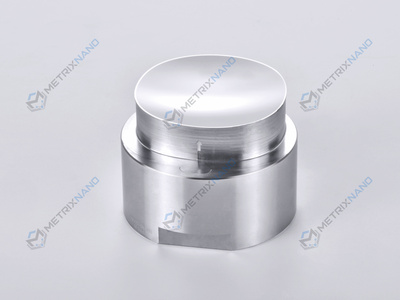
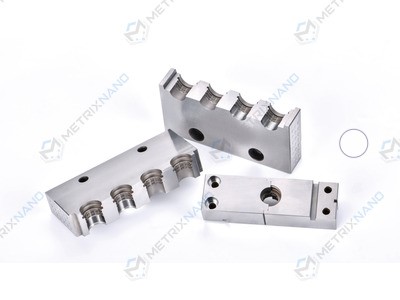
Thread Guide Plate — Precision guide component that meshes with the lead screw. Concentricity of the internal threads controls demolding stability. Inserted construction allows for individual replacement.
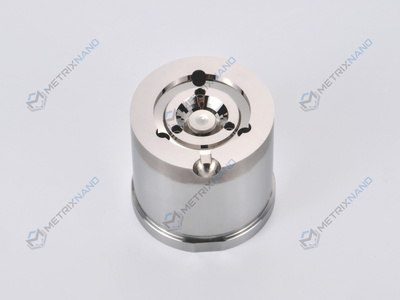
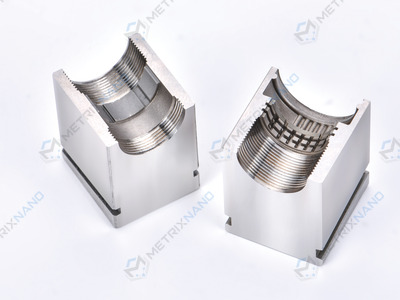
Cavity Insert — Forms the primary cavity profile. The lens barrel's external shape and snap-fit grooves are molded directly by this component. Machining precision reaches the micron level with mirror polishing.
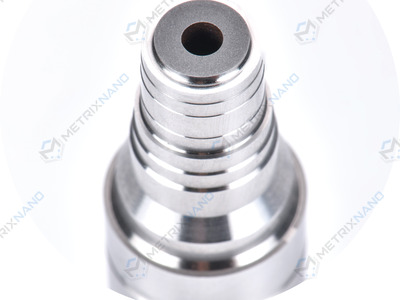
Core Pin — Forms fine internal features such as through-holes and light apertures. Made of S136 steel, with each dimensional step held to a tolerance of 0.001 μm. Ground with green silicon carbide abrasive to ensure superior surface quality.
Coordinated Workflow
Cavity insert and core pin establish the mold cavity → Threaded core pin is embedded to form internal threads → Injection filling, holding pressure, and cooling → Lead screw rotates under thread guide plate guidance to demold → All components reset for the next cycle. The five components are interlocked — any deviation in one will be amplified on the molded part.
Specifications
Component Function Diameter (mm) Height (mm) Heat Treatment Threaded Core Pin Internal thread forming Φ15–Φ35 30–100 S136, HRC 56 Lead Screw Rotary demolding Φ20–Φ40 50–120 Heat treatment, HRC 50–54 Thread Guide Plate Thread guidance Φ25–Φ45 30–80 Heat treatment, HRC 52–56 Cavity Insert Cavity forming Φ20–Φ50 40–120 Heat treatment, HRC 50–54 Core Pin Detail forming Φ15–Φ30 30–100 S136, HRC 56 Overall Range — Φ15–Φ50 30–120 — The core pin's step tolerance is held to 0.001 μm, meeting the stringent precision requirements of automotive lens barrels. Though small in size, these five components form the foundation of lens barrel molds — deep expertise in precision machining and process coordination is the key path to enhancing lens barrel quality.
— End —
Custom Ultra-Precision mold Manufacturer Europe | NDA Available | Engineering Response Within 24 Hours